Typically, when you contact Cleveland Punch & Die to get a quote or order tooling, we will ask you for the make and model number of the machine that these tools are going to be used in. We might also ask you for the numbering on the side of the tools that you currently have for that specific machine. What if you don’t have any of the above information? No worries! Take a look at the diagrams of the punch and die anatomies displayed below. You will need to identify the head diameter, body diameter and overall length of the punch and the outside diameter and height of the die. These measurements will allow us to determine the style of punch and die that your machine requires. If you need further assistance, you can call Cleveland Punch & Die @ (888)451-4342 from 7am-6pm Monday through Friday.
Monday, September 27, 2010
Monday, September 20, 2010
Punch End Configurations
The Cleveland Punch and Die Company offers our customers a variety of different punch end configurations. Each configuration is designed for a specific purpose and application to achieve the best quality hole possible. The punch ends offered by Cleveland Punch and Die include:
- Crown Edge with Center
- This is the standard punch end configuration on all of CPD's stock punches. It is used for general purpose punching and is great for locating the punch to a predetermined spot on the material (commonly marked with a center punch).
- Flat Face
- A flat face punch is frequently used to prevent the deformation of the piece of material that is being punched. Commonly referred to as a "blanking operation" many customers will generate a flat slug of material as a finished part.
- Full Crown
- A full crown punch end should be used when punching extremely hard material such as boiler plate. This punch end will help to keep the end of the punch intact and will strengthen the overall integrity of the punch while punching hard material.
- Chisel Point
- The most common use for a chisel point punch end is to reduce the tonnage of the punching application. This is useful when punching a large diameter hole on an ironworker. Ordering a punch with a chisel point can reduce the tonnage of the application by up to 20% depending on material type and thickness. Give us a call for engineering assistance to discuss your specific application.
- Concave Shear/Crisscross Shear
- A concave or crisscross shear is common on the 28XX and 36TC tooling lines. This punch end helps to reduce the deformation on thin material by shearing the material from the outside of the punch toward the center.
Cleveland Punch and Die can manufacture any special punch end per our customer's request. Give us a call to discuss your punching application and let our 130 years of experience guide you in the right direction.
Monday, September 13, 2010
Ripping Punches
Over the years, we have had customers that want to punch an oblong hole that is longer than what their machine allows them to punch. Cleveland Punch & Die has a solution!!! We would like to introduce you to our “Ripping Punch!” A “Ripping Punch” allows you to generate an oblong hole beyond the capacity of your ironworker. First, punch a round hole the same size as the width of your oblong hole. Next, insert the guide of the ripping punch through the pre-punched hole and begin cycling the machine while feeding the material into the guide. The guide should be 1/8” to ¼” longer than the material thickness. The material thickness should not exceed 3/8” A-36 mild steel.
For more information on the “Ripping Punch”, please contact one of our experienced “Green Team” members at (888)451-4342 from 7am-6pm Monday through Friday.
Tuesday, September 7, 2010
Countersink Punches and Dies
Cleveland Punch and Die manufactures tooling to countersink a wide variety of material. Our tools are designed to punch a hole in the material and form the material into a countersink, all in one operation. The "countersink and extrude" application is used when the material being punched/formed is thinner than 1/8". This set-up requires a countersinking punch and die to form the material properly. However, the "countersink and form" application, used when the material being punched is 1/8" or greater in thickness, can be used with a standard round die. These countersink tools will generate a standard 82° countersink in the material, a standard angle used throughout the industry.
Common products which use countersink tooling include truck beds, trailers as well as door and cabinet hinges. These products all require the head of a screw or bolt to sit flush with the material.
If you have a special countersink need, give us a call and let one of our experienced Sales Engineers design the perfect tools for your machine and application. We are available to assist your needs 7am-6pm, or you can email us at sales@clevelandpunch.com
Common products which use countersink tooling include truck beds, trailers as well as door and cabinet hinges. These products all require the head of a screw or bolt to sit flush with the material.
If you have a special countersink need, give us a call and let one of our experienced Sales Engineers design the perfect tools for your machine and application. We are available to assist your needs 7am-6pm, or you can email us at sales@clevelandpunch.com
Friday, August 27, 2010
Pipe Notch Tooling
ATTENTION all fabricators who need to cope or “fish mouth” the ends of tube or pipe…The Cleveland Punch & Die Company has the perfect set up for you! We have a variety of pipe notcher housings, tooling and striker punches in stock!!
These housings are perfect for ironworkers because you can remove your die block from your punching station and set up the striker punch in place of your regular punch. Don’t have an ironworker??? No Problem!! The pipe notcher assembly is a self-contained unit that can be used on any hydraulic or mechanically operated machine, as long as it has a bed that can secure the housing and a ram to strike the top of the tooling. The standard pipe notch housing is designed to accept punch and die assemblies up to and including 2-1/2” outside dimensions. A separate punch and die is required for each outside dimension along with a standard striker punch.
Typical end users can be found in the following industries: Automotive, Furniture, Motorcycle, Hand Railing, Scaffolding, Livestock, Fencing, Wrought Iron, Exercise, Medical and Aircraft. If you would like additional information regarding pipe notch tooling, we encourage you to contact one of our “Green Team” members for assistance! We can be reached Monday thru Friday, 7am - 6pm at 888-451-4342 or via email at sales@clevelandpunch.com.
These housings are perfect for ironworkers because you can remove your die block from your punching station and set up the striker punch in place of your regular punch. Don’t have an ironworker??? No Problem!! The pipe notcher assembly is a self-contained unit that can be used on any hydraulic or mechanically operated machine, as long as it has a bed that can secure the housing and a ram to strike the top of the tooling. The standard pipe notch housing is designed to accept punch and die assemblies up to and including 2-1/2” outside dimensions. A separate punch and die is required for each outside dimension along with a standard striker punch.
Typical end users can be found in the following industries: Automotive, Furniture, Motorcycle, Hand Railing, Scaffolding, Livestock, Fencing, Wrought Iron, Exercise, Medical and Aircraft. If you would like additional information regarding pipe notch tooling, we encourage you to contact one of our “Green Team” members for assistance! We can be reached Monday thru Friday, 7am - 6pm at 888-451-4342 or via email at sales@clevelandpunch.com.
Friday, August 20, 2010
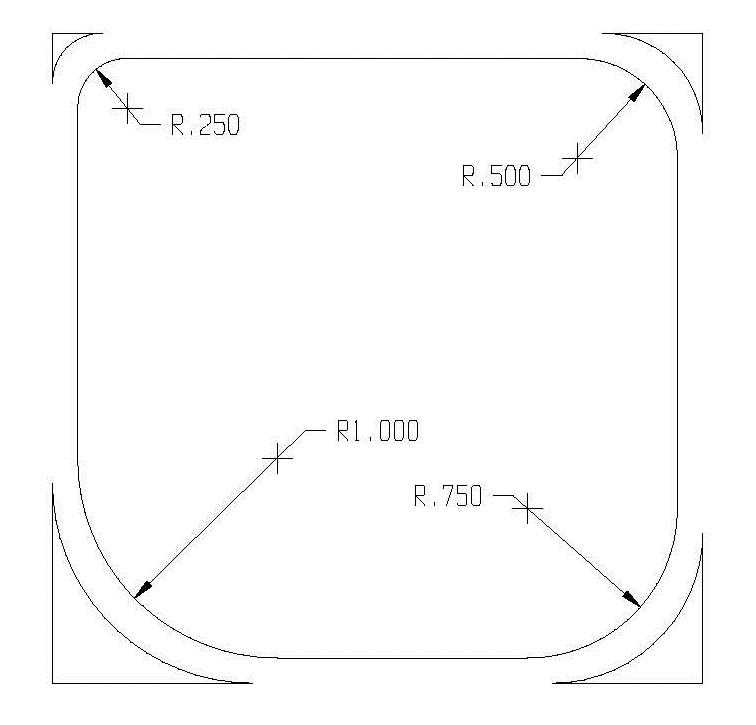
28XX Multiple Corner Radius Tool
Are you a manufacturer of signs? Are you a fabricator concerned about the hazard of rough corners? Maybe you already use our Corner Radius tooling, but would benefit from multiple radii. Then the Cleveland Punch & Die Company’s Multiple Corner Rounding Tool could be what you need. This tool has all the same benefits as our popular Corner Radius tooling but with even more flexibility. Imagine a single Corner Radius punch and die set and multiply it by four. That’s right, four radii on one punch and die! This reduces labor due to costly changeover of tooling, and at the same time is much more efficient when a job requires multiple radii. Give us a call today and let us design a multiple corner radius tool for your specific application.
Thursday, August 12, 2010
Geka Cluster Punch Application
Are you tired of punching multiple holes one at a time? What about the time required for set up or the labor hours incurred? If this gets you thinking, then you need to ask us about a cluster punch application!! Customers are finding that it is less time-consuming and not as expensive in the long run, to punch multiple holes at the same time!
Cleveland Punch & Die has just made a quad cluster die block that holds four F-59 oblong dies to be used in a Geka Hydrocrop 110. This customer is punching four oblong holes in a 6” x 15 lbs. W beam which is ¼” thick. These are used as connecting beams which is displayed below.
Please feel free to contact our experienced engineers for additional information regarding our cluster punches. We can be reached Monday thru Friday, 7am - 6pm at 888-451-4342 or via email at sales@clevelandpunch.com.
Cleveland Punch & Die has just made a quad cluster die block that holds four F-59 oblong dies to be used in a Geka Hydrocrop 110. This customer is punching four oblong holes in a 6” x 15 lbs. W beam which is ¼” thick. These are used as connecting beams which is displayed below.
Please feel free to contact our experienced engineers for additional information regarding our cluster punches. We can be reached Monday thru Friday, 7am - 6pm at 888-451-4342 or via email at sales@clevelandpunch.com.
Subscribe to:
Posts (Atom)